Handling Hazardous Fluids Safely with Sealless Canned Pump Technology
October 9, 2026
Selecting the right pumping technology is a critical decision for industries where reliability, safety, and continuous operation are essential. While conventional pumps have been widely used across industries for decades, modern applications involving hazardous, corrosive, or valuable fluids require advanced solutions that offer improved containment and operational reliability.
At Hydrodyne Teikoku, we have been manufacturing advanced pumping solutions for over two decades, helping industries achieve safer and more efficient fluid handling. Our canned pump technology is designed to overcome several limitations associated with traditional pumping systems, especially in applications where leakage prevention and reliability are key priorities.
Understanding the differences between canned motor pumps and conventional pumps helps industries select the right solution based on their process requirements.
Understanding Conventional Pump Technology
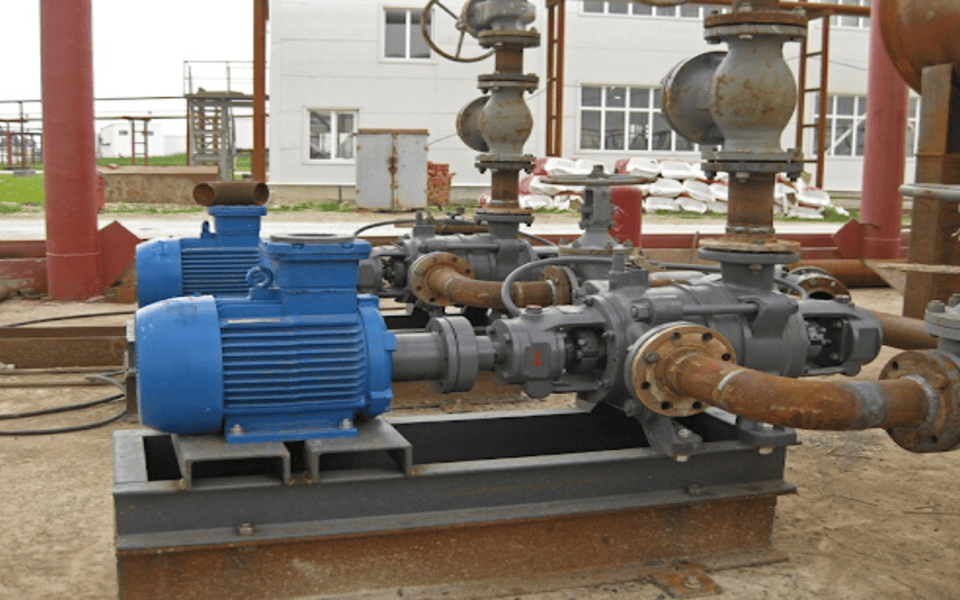
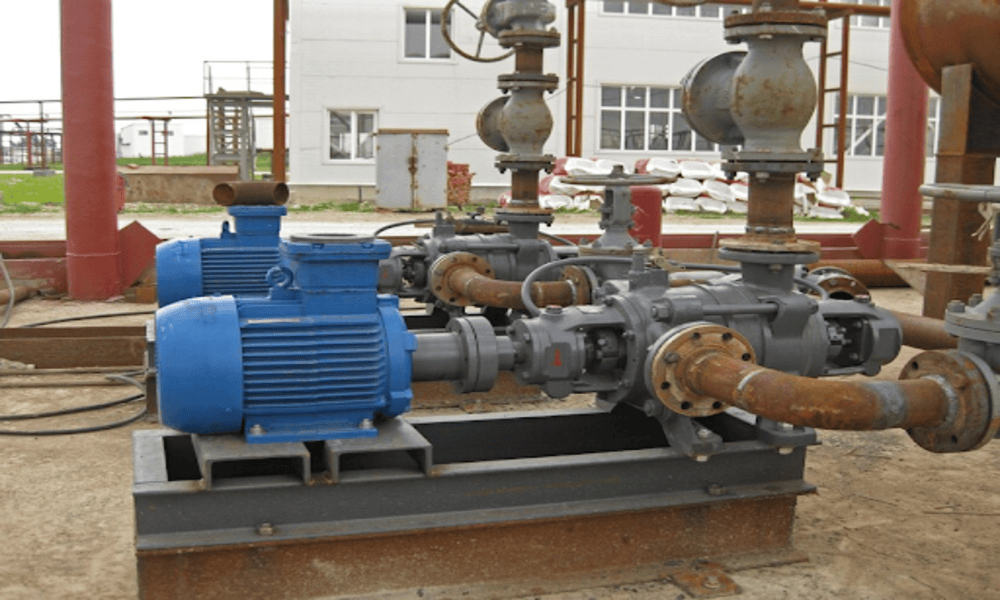
Conventional pumps have been used extensively in industrial applications due to their versatility and availability. These systems generally consist of a separate pump and motor connected through a coupling arrangement.
To prevent fluid leakage around the rotating shaft, conventional pumps typically rely on mechanical seals or packing systems. While these designs are suitable for many applications, mechanical seals are components that experience wear over time due to friction, pressure differences, temperature variations, and continuous operation.
In applications involving hazardous chemicals, flammable fluids, or environmentally sensitive liquids, seal performance becomes a critical consideration.
What Makes Canned Motor Pumps Different?
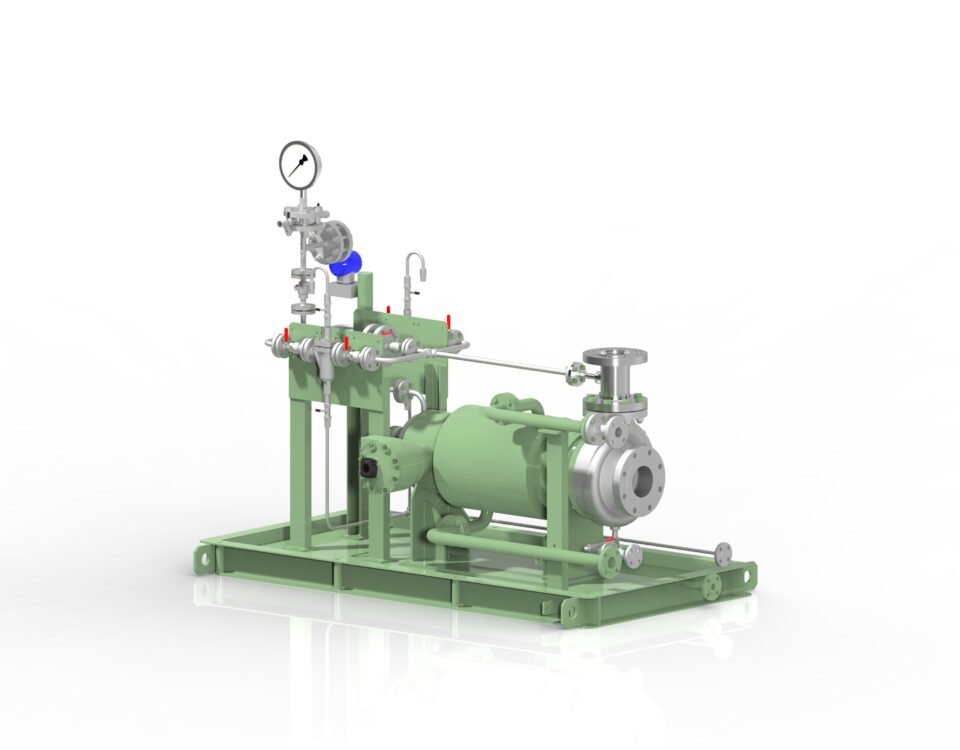
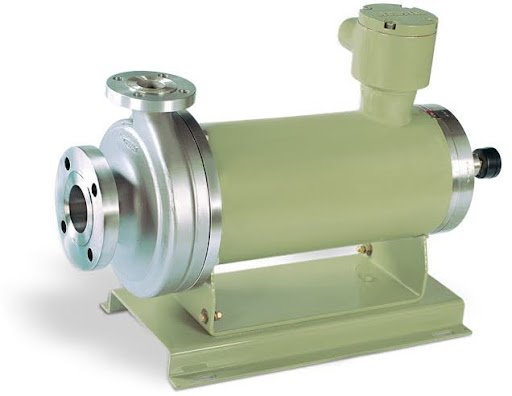
A canned pump uses a completely enclosed design where the pump and motor are integrated into a single unit. Unlike conventional pumps, this design eliminates the requirement for an external shaft seal.
The motor and pump operate within the same pressure boundary, creating a hermetically sealed system that helps prevent fluid exposure to the atmosphere.
This hermetically sealed canned motor pump technology provides industries with a reliable solution for applications where leakage prevention, safety, and process integrity are important. Hydrodyne Teikoku
Canned Motor Pumps vs Conventional Pumps: Key Differences
1. Leakage Prevention and Fluid Containment
One of the biggest differences between canned motor pumps and conventional pumps is the approach to leakage control.
Conventional pumps use mechanical seals to prevent fluid from escaping through the rotating shaft. Over time, seal wear can increase maintenance requirements and create potential leakage concerns.
A canned motor pump removes this external sealing point through its integrated construction. This makes it particularly suitable for industries handling toxic, volatile, corrosive, or high-value fluids.
Hydrodyne Teikoku’s leak-free pumping solutions are designed for applications where maintaining fluid containment is essential.
2. Design and Construction
Conventional pumps usually have separate motor and pump assemblies connected through couplings. This arrangement requires proper alignment between components for reliable operation.
Canned motor pumps combine the motor and pump into one compact assembly. Since there is no external coupling or shaft seal, the overall design is simpler and requires less space.
The integrated structure also reduces potential failure points associated with external mechanical components.
3. Maintenance Requirements
Maintenance requirements are an important factor when selecting industrial equipment.
In conventional pumps, mechanical seals require regular inspection and replacement depending on operating conditions. Seal failures can lead to unexpected downtime and production interruptions.
Because canned motor pumps eliminate mechanical shaft seals, they can significantly reduce seal-related maintenance activities. However, proper application selection, installation, and operating practices remain important for achieving reliable performance.
4. Safety in Hazardous Applications
Industries such as chemicals, petrochemicals, pharmaceuticals, and refrigeration often handle fluids that require strict safety controls.
For these applications, reducing the possibility of leakage is a major operational priority.
Hydrodyne Teikoku designs sealless canned pump solutions for industries where safe handling of critical fluids is required.
These pumps are widely considered for applications involving hazardous media because their enclosed construction helps improve containment and operational safety.
5. Application Suitability
Both conventional pumps and canned motor pumps have their own areas of application. Conventional pumps remain suitable for many general-purpose fluid transfer requirements.
However, industries working with demanding process conditions often require specialised solutions.
Canned motor pumps are commonly used in:
- Chemical processing plants
- Petrochemical facilities
- Pharmaceutical manufacturing
- Refrigeration systems
- Nuclear power applications
- High-temperature and high-pressure processes
Hydrodyne Teikoku provides application-focused solutions for sectors such as chemical industries, where reliable and safe fluid transfer is essential.
Why Industries Choose Canned Motor Pump Technology
The decision between conventional pumps and canned motor pumps depends on the application requirements, operating environment, and safety considerations.
For critical applications, industries often look beyond initial equipment costs and consider factors such as reliability, maintenance requirements, downtime risks, and environmental responsibilities.
Modern API 685 canned motor pumps provide industries with advanced sealless technology designed for demanding applications where conventional sealing systems may not be suitable.
Hydrodyne Teikoku: Delivering Advanced Pumping Solutions
At Hydrodyne Teikoku, we combine engineering expertise, manufacturing experience, and application knowledge to develop reliable pumping solutions for industries worldwide.
With decades of experience in canned motor pump technology, we understand that every application has unique challenges. Our engineers study operating conditions, fluid characteristics, temperature requirements, and pressure conditions to recommend the most suitable pump configuration.
From chemical processing and refrigeration to specialised industrial applications, our Hydrodyne Teikoku canned motor pumps are designed to deliver safe, reliable, and efficient performance.
Choosing the right pump technology is not only about moving fluids, it is about ensuring safer operations, improved reliability, and long-term value for industrial processes.