Chemical Pumps for Air Pollution Control Systems
August 31, 2026
Canned Motor Pumps vs. Conventional Pumps: Key Differences Explained
October 9, 2026
In industries where hazardous, toxic, volatile, or highly valuable fluids are transferred, pump selection is not only about achieving the required flow rate and pressure. It is also about ensuring safety, protecting the environment, and maintaining uninterrupted operations.
At Hydrodyne Teikoku, we understand the challenges industries face while handling critical fluids. For over two decades, we have been designing and manufacturing advanced pumping solutions that help industries achieve safe and reliable fluid transfer. Our sealless canned pump technology is developed to address one of the biggest concerns in industrial pumping preventing leakage of hazardous fluids.
When industries deal with chemicals, hydrocarbons, refrigerants, or other sensitive liquids, even a small leakage can impact workplace safety, product quality, and environmental compliance. This makes sealless pumping technology an essential solution for modern industrial applications.
Why Sealless Canned Pump Technology is Important for Hazardous Fluid Handling
Traditional pumping systems generally use mechanical seals to prevent process fluids from escaping. However, mechanical seals are one of the most critical components in a pump and can experience wear due to continuous operation, temperature variations, pressure changes, and demanding process conditions.
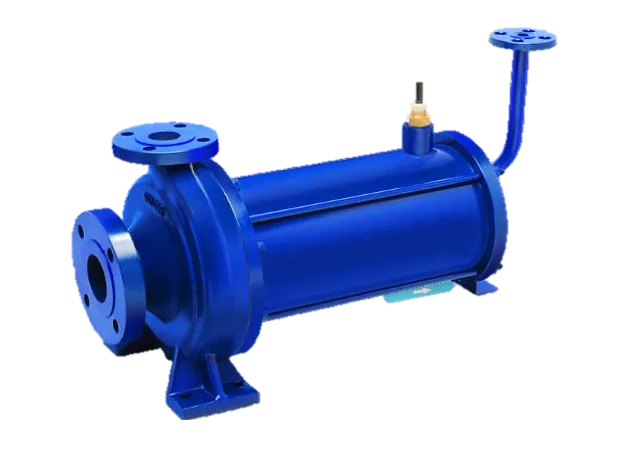
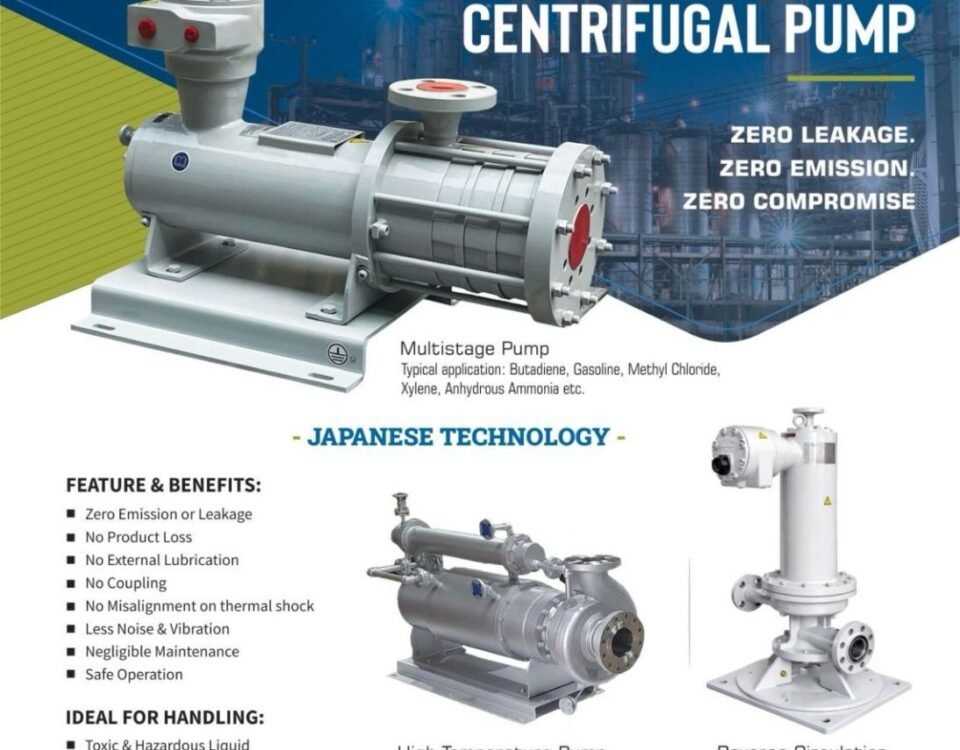
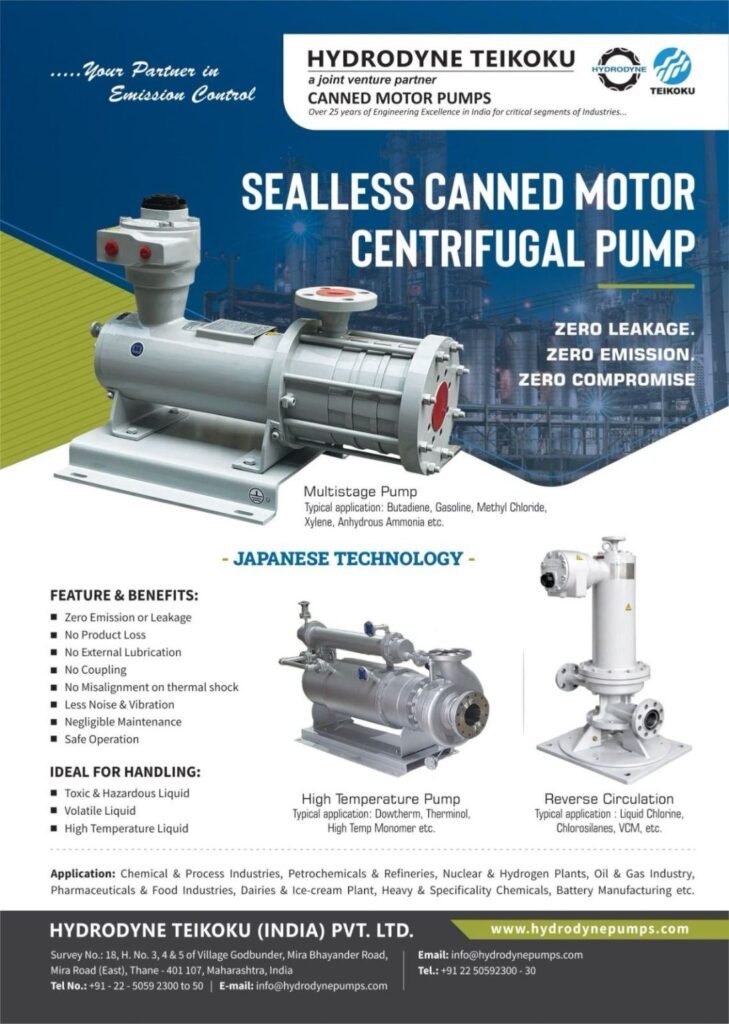
A sealless canned pump eliminates the requirement for a conventional mechanical shaft seal by integrating the motor and pump into a completely enclosed unit.
This canned motor pump technology creates a hermetically sealed system where the pumped fluid remains contained, reducing the possibility of external leakage.
For industries handling hazardous fluids, this design provides an additional level of safety by reducing emission risks and supporting more reliable plant operations.
How Sealless Canned Pumps Improve Industrial Safety
The biggest advantage of a sealless design is the elimination of the rotating shaft seal, which is traditionally considered a potential leakage point.
In a canned motor pump, the motor rotor and pump assembly are contained within the same pressure boundary. This compact construction helps maintain fluid containment while allowing the pump to operate efficiently in demanding applications.
At Hydrodyne Teikoku, our pump designs focus on:
- Safe handling of hazardous and corrosive fluids
- Reduced risk of fugitive emissions
- Reliable operation under extreme temperatures and pressures
- Lower maintenance requirements compared to conventional sealing systems
For industries where fluid containment is critical, choosing the right pumping technology can significantly improve operational safety.
Chemical Industry: Managing Corrosive and Hazardous Fluids
Chemical processing plants often handle aggressive chemicals, solvents, acids, and other hazardous media. These fluids require pumping systems that can maintain reliable performance while preventing unwanted exposure.
Our solutions for chemical industry applications are designed to support industries where safety and reliability are key requirements.
Sealless canned pumps are particularly valuable in chemical applications because they reduce leakage concerns associated with traditional sealing arrangements. This helps industries improve process safety while maintaining efficient fluid transfer.
From specialty chemicals to petrochemical processes, reliable containment plays an important role in protecting both employees and the surrounding environment.
Oil & Gas Applications: Reliable Pumping Under Challenging Conditions
The oil and gas sector operates with some of the most demanding fluid handling requirements. Facilities often transfer flammable hydrocarbons, volatile liquids, and high-value process fluids where leakage prevention is extremely important.
For such applications, API 685 canned motor pumps provide a reliable solution by following recognised industry requirements for sealless pump applications.
At Hydrodyne Teikoku, we design pumps that support critical operations where safety, reliability, and continuous performance are essential.
Pharmaceutical and Food Processing: Maintaining Process Integrity
Industries such as pharmaceuticals and food processing require high levels of cleanliness and process control. Any contamination or leakage can affect product quality and operational efficiency.
The enclosed design of sealless canned pumps supports cleaner and safer fluid handling by reducing external leakage points.
Our solutions for pharmaceutical and food industries help manufacturers maintain reliable processes while meeting the demanding requirements of these industries.
Refrigeration Systems: Safe Handling of Refrigerants
Industrial refrigeration systems require pumps that can safely circulate refrigerants under challenging operating conditions. Fluids such as ammonia require specialised equipment because leakage can create safety concerns.
Hydrodyne Teikoku provides dedicated refrigeration pump solutions designed for reliable operation in cold storage facilities and industrial cooling systems.
The sealless design helps maintain secure fluid containment, making it suitable for applications where refrigerant leakage prevention is a priority.
Beyond Safety: Reducing Maintenance and Improving Reliability
Safety is one of the primary reasons industries adopt sealless pumping technology, but the benefits extend further.
By removing mechanical seals, sealless canned pumps can reduce seal replacement requirements and help minimise maintenance interruptions. This allows industries to focus on improving uptime and operational efficiency.
Our leak-free pumping solutions are developed to support industries looking for dependable performance in critical applications.
Hydrodyne Teikoku: Engineering Safe Pumping Solutions for Critical Industries
At Hydrodyne Teikoku, we combine decades of engineering experience with advanced manufacturing practices to develop reliable pumping solutions for challenging industrial environments.
Our sealless canned pump technology supports applications across chemicals, petrochemicals, pharmaceuticals, refrigeration, nuclear power, and other specialised industries.
By understanding each application requirement, our engineers recommend suitable pump configurations, materials, and designs to ensure dependable long-term performance.
For industries looking for safe, reliable, and efficient fluid handling solutions, Hydrodyne Teikoku canned motor pumps provide proven technology designed for critical applications.